Support
 Request Testing
The Definitive Guide to Rapid Allergen Validation & Line Clearance

In high-throughput food manufacturing and co-packing, line clearance is the ultimate bottleneck. When a production line sits idle during an allergen changeover, it drains facility profitability by the minute. Yet, rushing the process is not an option. A single misstep in sanitation can lead to cross-contact, catastrophic Class I recalls, and irreparable brand damage.
Achieving operational efficiency requires a testing partner that pairs deep, rigorous allergen validation expertise with guaranteed, rapid turnaround times. Minimizing facility downtime relies on getting accurate, defensible data into the hands of Quality Assurance (QA) and Quality Control (QC) leaders exactly when they need it. Rapid data delivery mitigates regulatory risks, ensures compliance during unannounced third-party audits, and accelerates line clearance protocols so production can resume safely.
If your facility is operating under tight timelines, facing an upcoming audit, or experiencing costly product hold backlogs, immediate support is available.
Navigating High-Stakes Operational Pain Points
Food safety compliance is an operational and financial reality that impacts every level of a manufacturing organization. Different roles face distinct, high-stakes challenges when managing allergen control and line clearance.
Food Manufacturers: The Cost of Waiting
For proprietary food manufacturers, the financial and brand impacts of a Class I recall due to undeclared allergens are devastating. Beyond the immediate legal and recall logistics costs, the long-term erosion of consumer trust can permanently damage a brand’s market share.
On a daily operational level, traditional laboratory turnaround times create a different kind of financial strain: warehouse storage costs. Holding finished products on-site while waiting days for lab results chokes supply chains, delays order fulfillment, and ties up valuable working capital in stowed inventory.
QA/QC Leaders: The Burden of Proof
QA/QC leaders shoulder the constant stress of unannounced regulatory inspections or rigorous third-party audits from bodies governing standards like SQF, BRCGS, and FSSC 22000. Defending a sanitation program during an audit without fast, accessible data is an uphill battle.
This pressure is compounded when dealing with traditional, uncommunicative corporate laboratories. When a sample results window passes with zero transparency or direct access to the testing scientists, QA leaders are left in the dark, unable to make definitive operational decisions or answer auditor inquiries with confidence.
Co-Packers: The Scheduling Logistical Nightmare
Co-packers operate on razor-thin margins and dense production schedules, frequently running mixed-allergen profiles on shared equipment. The primary challenge is maintaining maximum line uptime while switching between completely different client formulations.
Cross-contamination penalties are a constant contractual threat. If a run for Client B is contaminated with an allergen from a previous run for Client A, the co-packer faces severe financial liabilities, broken contracts, and a damaged industry reputation. They require an agile sanitation and validation framework that supports rapid changeovers without sacrificing safety.
Educational Foundations: Validation vs. Verification
To build an unassailable food safety system, it is critical to understand the distinct legal and scientific definitions of validation and verification within an Allergen Control Plan (ACP).
An Allergen Control Plan (ACP) serves as the overarching strategy to prevent cross-contact from raw materials through to final packaging. Within this plan, facilities rely on two distinct pillars:
Method Validation:
This process legally and scientifically proves that a cleaning protocol is capable of working. It requires definitive laboratory analysis (using ELISA or DNA/PCR methodologies) to demonstrate that a specific sanitation process actually removes a targeted allergen from a specific piece of equipment or production matrix.
Sanitation Verification:
This process proves that a validated cleaning protocol was executed correctly during routine operations. It relies on immediate, daily line clearance checks—such as rapid, on-site lateral flow strips or ATP swabs—to verify cleanliness before restarting production.
Allergen Control Plans (ACP)
An Allergen Control Plan is a comprehensive, written systematic strategy designed to prevent allergen cross-contact at every stage of the manufacturing process. It dictates protocols from the moment raw ingredients arrive at the receiving dock, through storage segregation, scheduling matrixes, processing, sanitation, and final packaging. The ACP serves as the framework that regulatory bodies review to judge a facility’s preventive controls.

Sanitation Verification
Verification is the routine, day-to-day assessment showing that a sanitation protocol was executed correctly. It answers the question: Did we clean the line properly today according to our established plan?
This is typically achieved through rapid, on-site lateral flow strips or ATP swabs immediately following a washdown. While lateral flow strips provide excellent, immediate feedback for daily operational line clearance, they are screening tools with limitations in sensitivity and matrix compatibility. They do not replace formal validation.
Method Validation
Validation is the definitive, legally required proof that a specific sanitation process is scientifically capable of removing a targeted allergen from a specific piece of equipment or production matrix. It answers the question: Does our cleaning protocol actually work?
Validation requires highly sensitive, specialized laboratory methodologies, such as Enzyme-Linked Immunosorbent Assay (ELISA) or Polymerase Chain Reaction (PCR/DNA). Regulatory standards dictate that facilities must validate their cleaning processes whenever a new allergen is introduced, equipment is modified, or cleaning protocols change, ensuring that the limits of detection match or exceed safety thresholds.
Testing Capabilities, Methodologies & Matrix Optimization
Selecting the correct analytical tool depends heavily on the specific target allergen, the nature of the food matrix, and how the product has been processed.
The Big 9 and Beyond
Accurate testing requires established methodologies tailored to the specific proteins responsible for allergic reactions. Food safety regulations focus heavily on the “Big 9” allergens:

Milk

Egg

Peanut

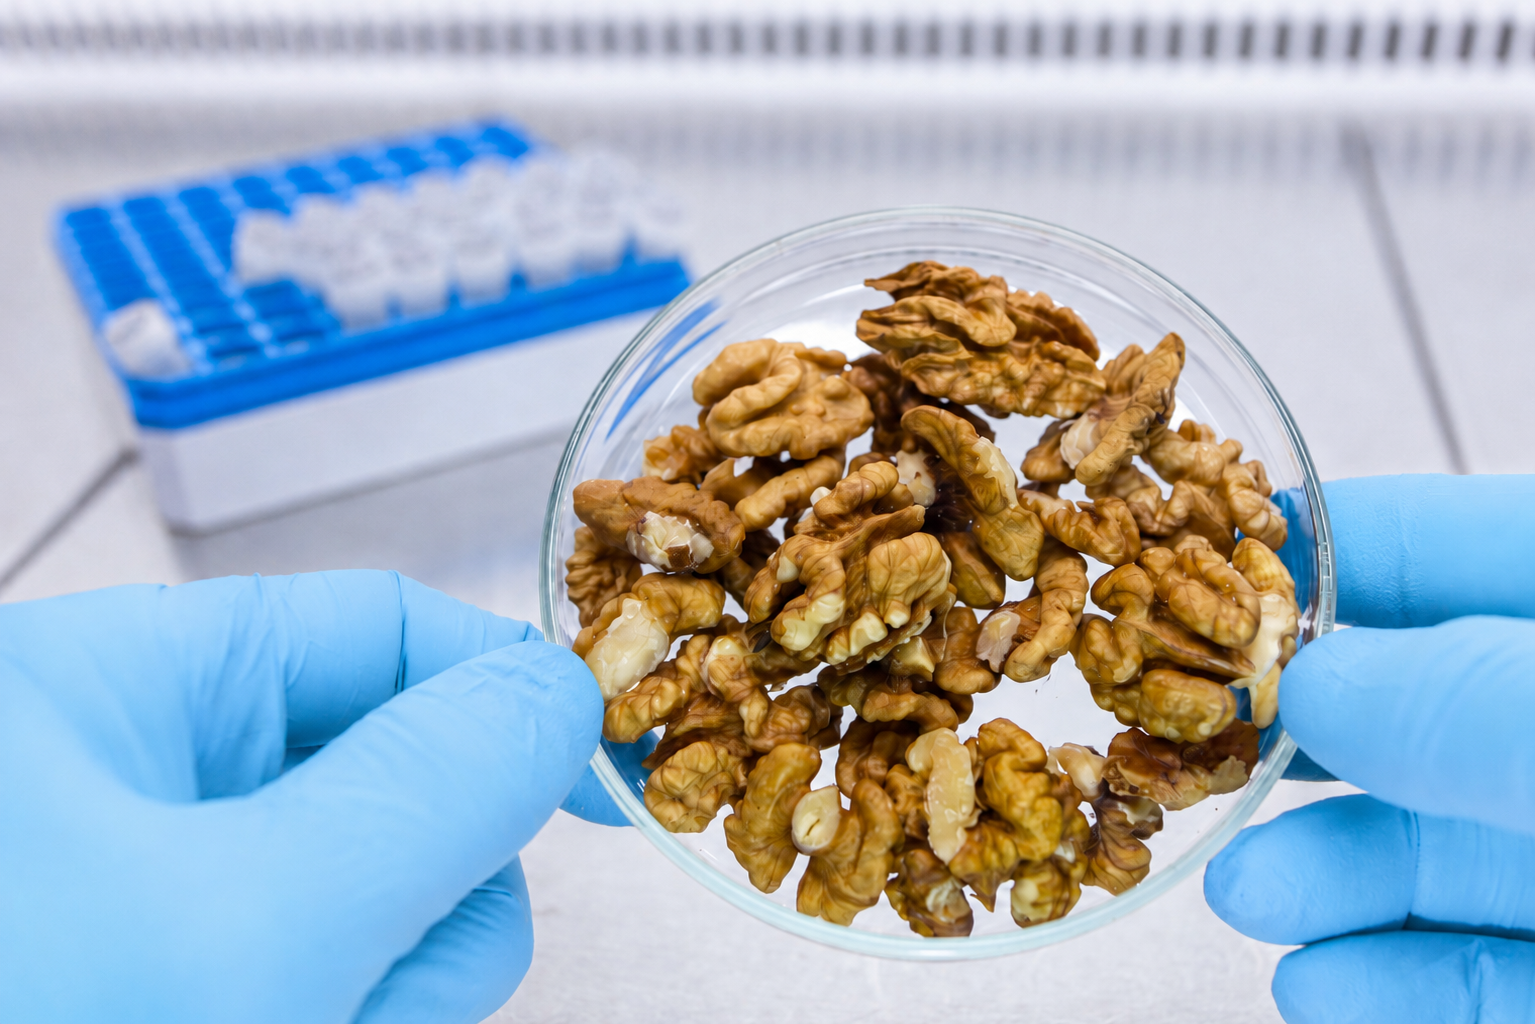
Tree Nuts (e.g., almond, walnut, cashew)

Wheat
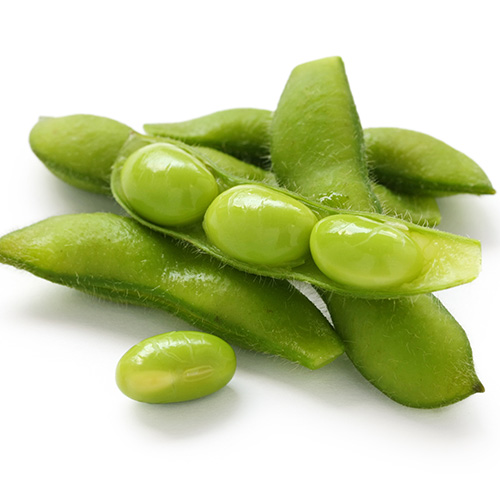
Soy

Fish
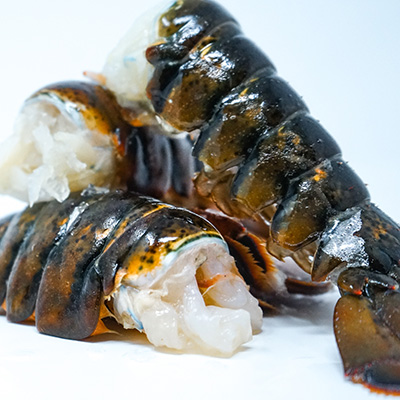
Shellfish (e.g., crustacean, mollusc)

Sesame
Optimizing Across Diverse Matrices
An allergen extraction method that works perfectly for a simple environmental surface swab will fail when applied to a complex food matrix. Laboratories must optimize testing protocols across four primary sample types:

Raw
Materials
Assessing incoming ingredients for undeclared allergens or supplier cross-contact before they enter production.

Environmental
Swabs
Sampling critical control points, niches, and hard-to-clean areas on processing machinery post-sanitation.
Rinse
Water
Analyzing the final CIP (Clean-in-Place) rinse water to ensure no residual allergen proteins remain suspended in the system.

Complex Finished Food Matrices
Evaluating final products that may contain highly processed, multi-ingredient, fat-heavy, or acidic components that can interfere with standard protein extractions.
Technology Applications: ELISA vs. DNA/PCR
Deploying the right technology depends on the state of the allergen protein within the sample matrix.
ELISA (Enzyme-Linked Immunosorbent Assay)
ELISA is the gold standard for most routine allergen testing. It works by using site-specific antibodies to detect and quantify the presence of specific allergen proteins. It is highly effective for raw materials, environmental swabs, and minimally processed foods.
However, if an allergen protein has been severely denatured, degraded, or altered by extreme heat, pressure, or fermentation, the antibodies in an ELISA test may no longer recognize it, potentially yielding a false negative.
DNA/PCR (Polymerase Chain Reaction)
When proteins are highly processed or altered, or cross reactivity issues arise with the standard ELISA testing methods, DNA-based testing (PCR) is often the superior choice.
Instead of searching for the protein itself, PCR amplifies and detects specific DNA sequences unique to the allergen source (such as detecting soy DNA in a highly processed lecithin or refined oil).
While PCR cannot easily measure the exact amount of allergen protein present, it provides an ultra-sensitive, definitive yes/no answer regarding the presence of the allergen source material, making it an essential tool for verifying line clearance in complex chemical or thermal processing environments.
Compliance, Audits, and Rigorous Reporting
When an enforcement officer or third-party auditor steps onto the production floor, guesswork is a liability. Survival depends on transparent, defensible, and easily accessible data.
Defensible Data Under Scrutiny
Data must be strong enough to withstand intense scrutiny from the FDA, USDA, and third-party auditing bodies (such as SQF or BRCGS). This means the testing laboratory must adhere to strict quality control parameters, utilize validated and peer-reviewed testing methods, and maintain impeccable chain-of-custody documentation. When a laboratory delivers a result, it must be legally and scientifically defensible under regulatory review.
Traceability and Digital Integration
Modern quality assurance demands speed not just in the lab, but in data transmission. Test results should integrate smoothly into modern QA Laboratory Information Management Systems (LIMS). Seamless digital data delivery allows QA managers to track allergen testing trends over time, map environmental monitoring results across facility blueprints, and instantly retrieve past data points during internal reviews.
Audit Defense with Bulletproof CoAs
The ultimate shield during a surprise compliance inspection is a bulletproof Certificate of Analysis (CoA). A proper CoA provides clear, unambiguous details: the specific sample tested, the method used, the limit of detection (LOD), the limit of quantification (LOQ), and the verified signatures of the analytical team. Presenting an organized history of clear, accredited CoAs immediately signals to an auditor that your facility’s allergen control and sanitation validation programs are under total control.
Real-World Operational Applications
Operational Optimization: Eliminating the Inventory Bottleneck
Consider a mid-sized bakery manufacturing facility that produces both standard and gluten-free/nut-free product lines. Under their traditional testing setup, the facility utilizes a local laboratory with a standard 5-to-7 business day turnaround time for allergen validation.
Because they cannot risk shipping a contaminated product, the facility is forced to hold every batch of finished goods in an on-site warehouse until the negative allergen CoAs arrive. This creates a severe logistics bottleneck, completely fills their warehouse capacity, and delays distribution to retail partners.
Under a traditional turnaround model, production on Day 1 requires shipping to a lab on Day 2, followed by several days of processing, leading to product release on Day 6. This results in five days of costly inventory hold.
By transitioning to an accelerated testing protocol with Microbac, sample pickup and processing are optimized. The impact is immediate: product hold times drop by over 60%, clearing warehouse gridlock, freeing up operational capital, and allowing the facility to scale up production runs without expanding its physical footprint.
Audit Intervention: Resolving a Sanitation Non-Conformance
During an unannounced BRCGS recertification audit, a Tier-1 co-packer is flagged for a critical non-conformance. The auditor notes that a newly installed automated seasoning conveyor line lacks sufficient historical allergen validation data for dairy and sesame proteins, threatening to downgrade the facility’s audit score and halt current client production runs. The quality director is given a strict 72-hour window to provide definitive scientific proof that the conveyor’s Clean-in-Place (CIP) cycle completely eradicates allergen residues.
The co-packer contacts Microbac’s technical team immediately. Microbac dispatches specialized environmental swab kits to the facility, receives the exposed samples under an expedited rush protocol, and deploys high-sensitivity ELISA testing.
Within 36 hours of the initial non-conformance flag, Microbac delivers a comprehensive, ISO-accredited data package and validated CoAs directly to the quality director. The data proves the sanitation cycle’s efficacy, allowing the team to confidently present the necessary evidence to the auditor, successfully clear the non-conformance, protect their AA audit rating, and prevent a catastrophic facility shutdown.
The Microbac Difference
Microbac does not operate as a distant, automated testing factory. We function as an agile, highly accessible extension of your facility’s internal quality assurance team.
Speed to Market
We understand that every hour a manufacturing line sits idle during an allergen changeover directly impacts your bottom line. Our testing networks are optimized for speed, offering expedited testing timelines that deliver accurate data
Technical Breadth
Microbac maintains an extensive suite of ISO/IEC 17025 accredited allergen tests across our laboratory network. With the capability to execute dozens of specialized allergen testing parameters, we handle complex matrix extractions and diverse validation setups that smaller regional labs simply cannot accommodate.
Direct Scientific Access
When a test result comes back positive or an auditor challenges an environmental monitoring data point, you cannot afford to navigate a tiered corporate call center or wait days for an email response. Microbac provides direct communication channels to the technical experts and scientists conducting your assays. You can speak directly with the testing team to troubleshoot matrix interferences, review raw data, and make high-stakes operational decisions with complete confidence.
Streamlined Onboarding and Next Steps
Low-Friction Onboarding
Our team manages the heavy lifting of transition planning. We analyze your current testing schedule, match your matrix profiles to our validated methods, provide specialized sample submission guidelines, and supply your QA team with standardized environmental sampling kits. Our streamlined onboarding ensures that your first sample batch moves seamlessly from your facility floor into our analytical system without data gaps or delays.
Expand Your Quality Resources
Allergen validation is only one component of a resilient food safety infrastructure. Microbac offers a complete suite of secondary technical assets and testing programs to protect your operations, including:
- Comprehensive Environmental Monitoring Programs (EMP) for pathogens
- Routine microbiological indicator testing (Aerobic Plate Count, Coliforms, Yeast & Mold)
- Expert-led technical consultations and facility vulnerability assessments

Need help determining the right allergen tests?
Not sure which allergen or testing method fits your product? Share the details Microbac needs to help determine the best next step and begin a faster, more informed testing process.
Take control of your facility uptime and secure the defensible data your brand requires.
Download and complete our Ingredient Submittal Questionnaire for Allergen Testing to initiate your rapid onboarding, or connect directly with a Microbac validation specialist to optimize your line clearance protocols today.